High-precision orthopedic instruments, surgical power tools, and implant solutions certified to global regulatory standards.
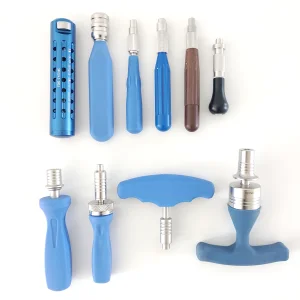
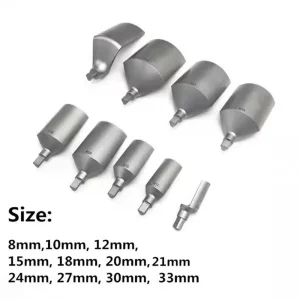
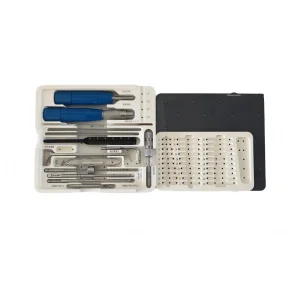
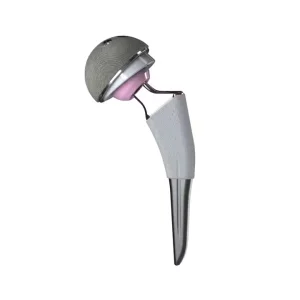
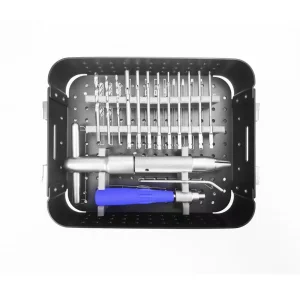
In modern critical care medicine, the division between high-precision mechanical tools and therapeutic gas-delivery systems has narrowed. High-performance respiratory care demands extreme tolerance manufacturing, precise volumetric control, and robust bio-compatible materials. As a premier hub for medical technology manufacturing, China's medical device industry has successfully leveraged its deep expertise in high-tolerance orthopedic devices—such as torque bone screwdrivers, complex spinal fixation systems, and specialized veterinary power saws—into the development of state-of-the-art respiratory support systems.
At the center of this technological intersection is Shenzhen HUL Healthcare Technology Co., Ltd. (also recognized globally under the brand Bopull Medical). Known for its strict adherence to international quality management frameworks, HUL Healthcare operates under the rigorous guidelines of the GB/T42061-2022 idt ISO13485:2016 international standard certification. By utilizing the same high-tier metallurgy and micro-machining workflows that produce titanium alloy implants and high-speed surgical drills, the company contributes critical component manufacturing capabilities and supply chain expertise to the respiratory ventilation sector.
This technical cross-compatibility is key. The mechanical valves, proportional solenoids, and turbine impellers used within modern Intensive Care Unit (ICU) ventilators require the exact same grade of sterile stainless steels and titanium alloys that are used in orthopedic bone screws and joint prostheses. Operating at tolerances measured in microns, our specialized technicians ensure that the gas paths in high-frequency oscillatory ventilators remain free of friction, dust, or toxic volatile organic compound (VOC) outgassings.
The technological trajectory of respiratory support devices is shifting toward intelligent, adaptive closed-loop systems powered by AI-driven diagnostics.
Next-generation medical ventilators incorporate closed-loop oxygen control (CLiO2). By measuring continuous arterial oxygen saturation (SpO2) via non-invasive sensors, the machine automatically adjusts the fractional inspired oxygen (FiO2) in real-time. This mitigates risks of hyperoxia and hypoxia, particularly in neonates and acute respiratory distress syndrome (ARDS) patients.
Traditional ventilators relied heavily on centralized wall-gas systems. Modern portable ICU-grade devices utilize ultra-quiet, brushless DC micro-turbines. These high-speed blowers spin up to 60,000 RPM, providing precise flow profiles (exceeding 300 L/min) while maintaining rapid acceleration curves to meet sudden, high-demand patient efforts.
Driven by the post-pandemic digital health acceleration, homecare CPAP and bi-level positive airway pressure (BiPAP) systems are transitioning to IoT cloud architectures. Clinicians can remotely monitor patient compliance, change pressure settings, evaluate Apnea-Hypopnea Index (AHI) data, and run remote predictive maintenance diagnostics.
Looking to the next decade, the industry is moving toward physiologically protective ventilation models. By combining high-frequency mechanical oscillation (HFOV) with artificial intelligence, systems can dynamically calculate the patient’s lung compliance and estimate recruitability. The ventilator will then suggest optimal positive end-expiratory pressure (PEEP) levels to prevent alveolar collapse without over-distending lung tissues.
A diverse portfolio of respiratory technologies configured for the unique operational environments of global medical systems.
Fully-featured critical care ventilators with high-flow nasal cannula (HFNC) modes, invasive & non-invasive ventilation, and lung mechanics monitoring modules.
Lightweight, ruggedized, battery-operated transport ventilators that resist shock, moisture, and high vibration. Ideal for first responders and air ambulances.
Automated CPAP/APAP devices, mobile oxygen concentrators, and respiratory humidifiers designed for patient compliance, quiet operations, and ergonomics.
Integrated vaporizers and ventilation bellows systems that ensure stable anesthetic agent titration and precise gas recycling loops inside operating rooms.
By coordinating with localized clinical networks, HUL Healthcare contributes its precision manufacturing capacity to optimize the production of these systems. With our verified engineering capabilities, we support OEMs globally in delivering parts that withstand continuous operations under demanding clinical schedules, matching the strict reliability metrics required in high-stress medical fields.
China's dominance in medical equipment manufacturing is no longer based solely on cost; it is built on industrial integration, supply chain resilience, and advanced automation. A prime example is our Shenzhen and Beijing operational footprint, which leverages local material-science ecosystems and world-class shipping hubs. Under the management of shenzhen HUL Healthcare Technology Co., Ltd. (Bopull Medical), our strategic supply partnerships and advanced production methodologies represent the cutting edge of Medical Device Industry 4.0.
Our production facilities integrate multi-axis CNC milling, automated laser welding, and Class 10,000 (ISO Class 7) cleanrooms to assemble complex, contamination-sensitive devices. We manage every step of the fabrication process—from raw material verification of medical-grade 304/316L stainless steels and titanium alloys to high-precision tolerance testing. In addition, our robust quality control protocols are backstopped by advanced Coordinate Measuring Machines (CMM) and digital vision sensors, ensuring zero-defect quality across every production run.
This factory-level efficiency directly benefits global buyers through shortened lead times. By utilizing local raw-material and component-sourcing ecosystems within China's premier industrial zones, we secure access to sensors, pumps, valves, and advanced electronics at low cost and stable lead times, mitigating supply chain shocks and shipping delays that impact other global manufacturers.
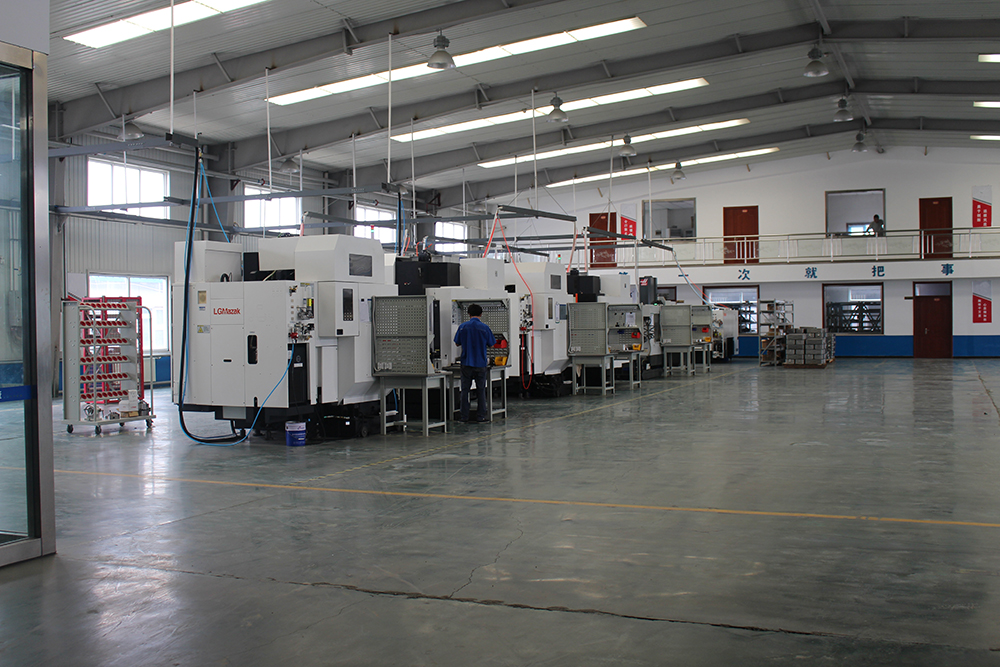
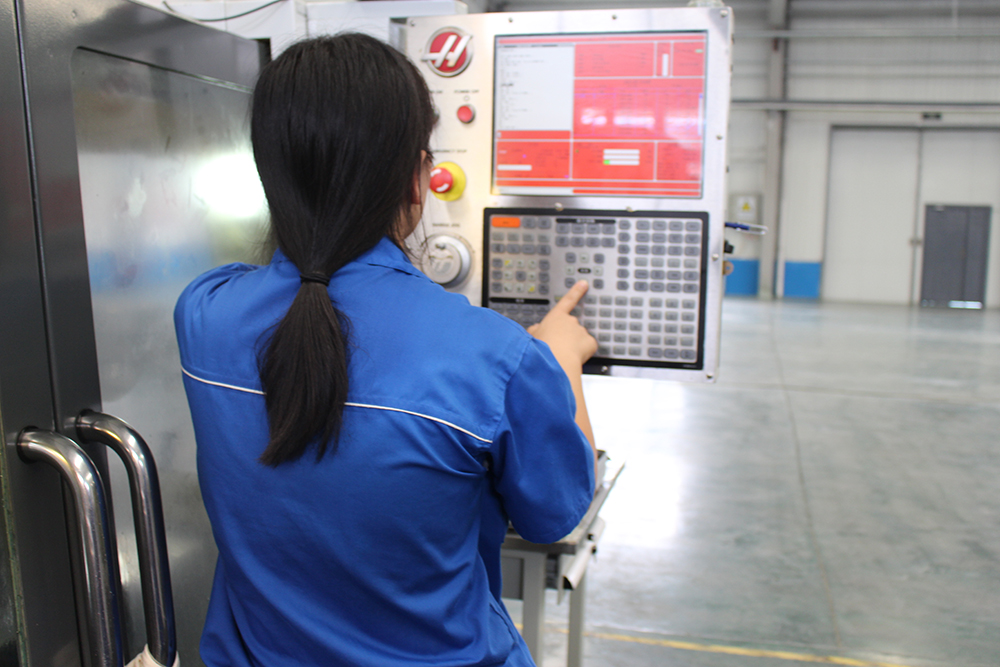
Procuring medical devices globally requires navigating a complex web of national regulations. HUL Healthcare prioritizes regulatory compliance, ensuring that all distributed components and finished assemblies meet the standards of major destination markets. By adhering to ISO 13485:2016 and maintaining CE and ISO certifications across our core orthopedic and surgical product lines (such as the TPLO surgical saws and titanium implant systems), we have built the institutional knowledge required to secure approvals for respiratory care equipment.
Our localized support structure focuses on key pillars:
Large-scale hospital networks, ministries of health, and international B2B distributors do not search simply for a low-cost vendor; they look for strategic partners that mitigate systemic operational risks. When sourcing advanced products like respiratory apparatuses, high-speed orthopedic tools, or internal fixators, procurement managers evaluate four main criteria:
Supply Chain Security: Global disruptions can impact clinical operations. A partner with diversified raw material suppliers, internal manufacturing depth, and a high annual revenue tier (US$1 Million - US$2.5 Million) ensures stable long-term operations. Our strong balance sheet and supply alliances shield partners from sudden price surges or supply shocks.
Rapid Technical Communication: In the medical field, a delay in resolving a technical query can stall clinical procedures. Bopull Medical maintains a response rate of 95.36%, with response times typically under 3 hours. This guarantees that engineering and procurement queries receive prompt answers from trained professionals.
Repeatable Quality: The 34% reorder rate highlights the trust global clients place in our consistency. Repeat business in medical device sectors is earned through consistent batch-to-batch quality, precise mechanical tolerances, and reliable long-term performance.
Technical responses and purchasing guidelines for international procurement managers.
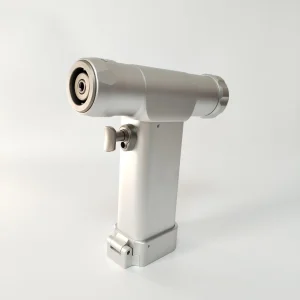
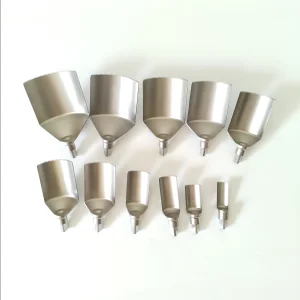
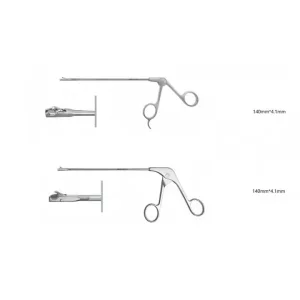
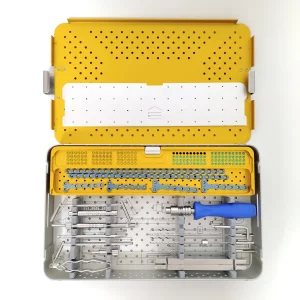
Advanced veterinary tools, arthroscopic forceps, and implant components engineered for demanding clinical applications.
 HUL Healthcare Limited