High-precision orthopedic, neurological, and general surgery instruments manufactured to strict EU MDR criteria.
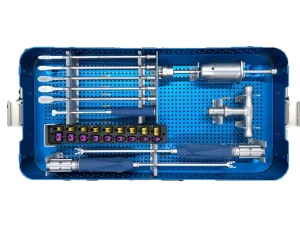
In recent years, the medical technology landscape in Eastern Europe, particularly in Romania, has undergone a profound transformation. Historically serving as downstream consumers of Western European medical technologies, surgical centers and medical institutions in Romanian cities like Bucharest, Cluj-Napoca, Timișoara, and Iași are now actively integrating into global production and supply networks. The demand for high-grade surgical instrumentation has escalated, driven by modernization projects in local hospitals, the expansion of private healthcare clinics (such as Regina Maria and MedLife networks), and a booming veterinary orthopedics sector.
While Romania has localized manufacturing capacity in general metalwork and automotive engineering, highly specialized medical-grade surgical instruments require advanced materials like vacuum-melted 316LVM stainless steel, Ti-6Al-4V ELI titanium alloys, and shape-memory Nitinol. Modern surgery instrument factories in Romania rely heavily on strategic supply chain collaborations with advanced OEM/ODM partners in global manufacturing hubs like Shenzhen. By leveraging global logistics networks and localized quality control mechanisms, Romanian distributors can secure instruments that meet the stringent European Medical Device Regulation (EU MDR 2017/745) requirements while maintaining competitive procurement pricing.
The global surgical instrument industry is experiencing a post-pandemic realignment characterized by two dominant trends: localized supply resilience and strict clinical efficiency requirements. Hospital administrations in Romania face the challenge of cost-containment alongside a push toward Minimally Invasive Surgery (MIS) techniques. MIS procedures, such as OLIF (Oblique Lateral Interbody Fusion) and laparoscopic interventions, require instruments with extremely low mechanical tolerances. For instance, the OLIF Tubular Retractor systems must provide reliable tissue exposure while minimizing surgical trauma, demanding high-grade mechanical strength and structural integrity.
To address these needs, surgical instrument factories must deploy a integrated engineering approach. This involves CAD/CAM design matching, rapid prototyping, and sophisticated surface finishing (such as physical vapor deposition - PVD - and electrochemical passivation). Passivation is critical as it enhances the chromium oxide layer on stainless steel, protecting instruments against pitting and stress corrosion cracking during repeated autoclave cycles. By bridging the manufacturing expertise of China with local European distribution networks, HUL Healthcare enables hospitals in Romania to access specialized orthopedic and veterinary surgical kits without the premium markups typical of traditional Western European suppliers.
Each instrument batch is delivered with full traceability certificates, material composition breakdowns, and CE certification aligned with the EU MDR, ensuring hassle-free importation and clinical validation within Romania.
We support Romanian distributors and surgical brands by modifying dimensional metrics, torque limiters, and instrument surface coatings (e.g., Titanium Nitride for improved wear resistance) to suit specific clinical workflows.
Our global support team provides 24/7 technical assistance. We offer detailed operation manuals, sterilization guides, and video tutorials for complex instruments, ensuring optimal lifecycle management.
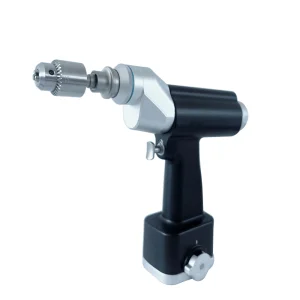
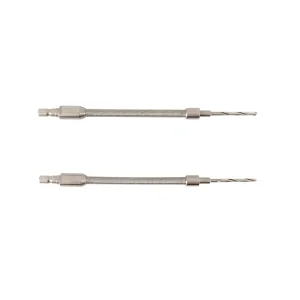
The integrity of a surgical instrument relies heavily on its metallurgical profile. In orthopedic procedures involving heavy impaction, bone cutting, and drilling, the instruments are subjected to extreme torsional stresses. We utilize high-grade, vacuum-arc remelted (VAR) stainless steel alloys, which offer superior micro-cleanliness, minimal non-metallic inclusion content, and exceptionally uniform grain structures. This material strategy ensures our orthopedic surgical bone drills and flexible reamers resist fatigue and mechanical deformation over extended usage cycles.
Furthermore, our sports medicine devices utilize Nitinol (Ni-Ti alloy) wire, which exhibits unique thermo-elastic shape-memory and superelastic properties. At body temperature, Nitinol instruments can undergo massive elastic deformations and return to their pre-formed shapes. This mechanical profile is essential for modern surgical sutures, flexible guide wires, and tendon repair tools, enabling Romanian orthopedic specialists to perform intricate joint reconstructions with minimal incisions.
Romania has seen a substantial rise in veterinary clinics, particularly dedicated to high-end small and large animal orthopedic procedures. Companion animal diagnostics and fracture repairs require specialized veterinary surgical kits. Because canine and feline anatomy varies dramatically from human bone density and structure, veterinary clinics in regions like Cluj and Brașov require orthopedic locking plates, Pearl plates (SOP system), and torque-controlled bone screwdrivers.
Our ALPS titanium locking plate and veterinary systems are engineered precisely for these settings. Manufactured from biocompatible titanium alloys (which minimize tissue reaction and accelerate bone integration), these systems feature adjustable configurations that adapt to dynamic veterinary clinical needs. The inclusion of precise syringes, torque control handles, and dedicated implant screws ensures veterinary surgeons in Romania can achieve the same level of anatomical stability and biomechanical performance in animal care as is expected in human orthopedics.
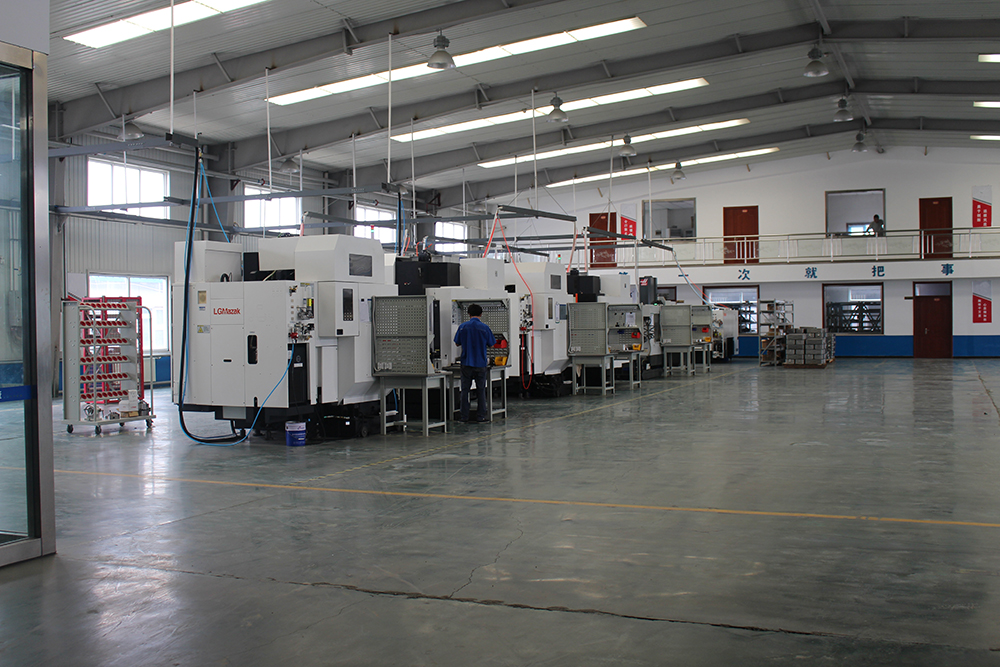
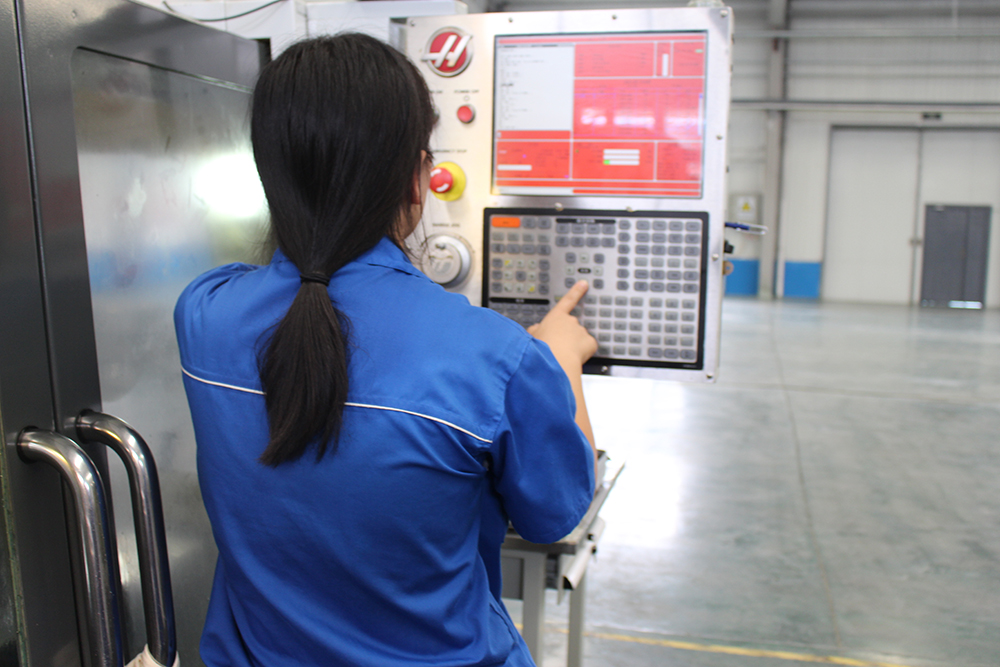
The horizon of surgical instrument manufacturing is shifting toward smart, sensor-integrated tools and sustainable production. We are actively developing next-generation medical drills and screwdrivers that incorporate IoT tracking modules and torque-overload alert systems. These smart surgical devices can record data from individual surgeries—such as heat generated during bone drilling and peak torque applied during screw seating—to optimize surgical safety and track tool wear over time.
Additionally, the transition to sustainable metal fabrication processes is a priority. Our manufacturing facilities are progressively incorporating laser powder bed fusion (LPBF) 3D printing technologies to produce customized surgical guides and patient-specific implants directly from medical CT data. By digitizing the design pathway, we can rapidly customize instruments and send digital manufacturing templates to local distribution partners in Romania, laying the groundwork for a more agile, decentralized, and environmentally friendly medical device supply chain.
Designed for reliability, durability, and high surgical performance. All items include factory warrenties and CE clearance.
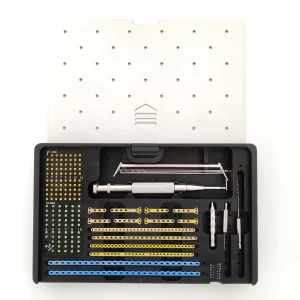
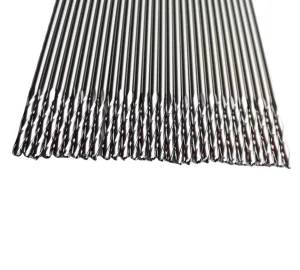
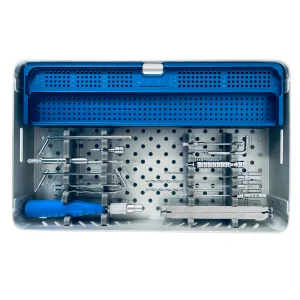
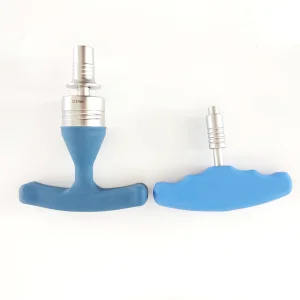
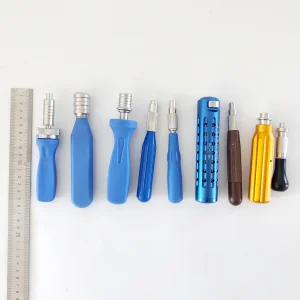
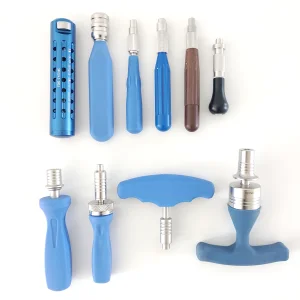
Shenzhen HUL Healthcare Technology Co., Ltd. (Bopull Medical) serves as the primary manufacturer and supply partner for international surgical supply brands.
Essential information concerning importation, certification, and customization of surgical instruments in Romania.
 HUL Healthcare Limited